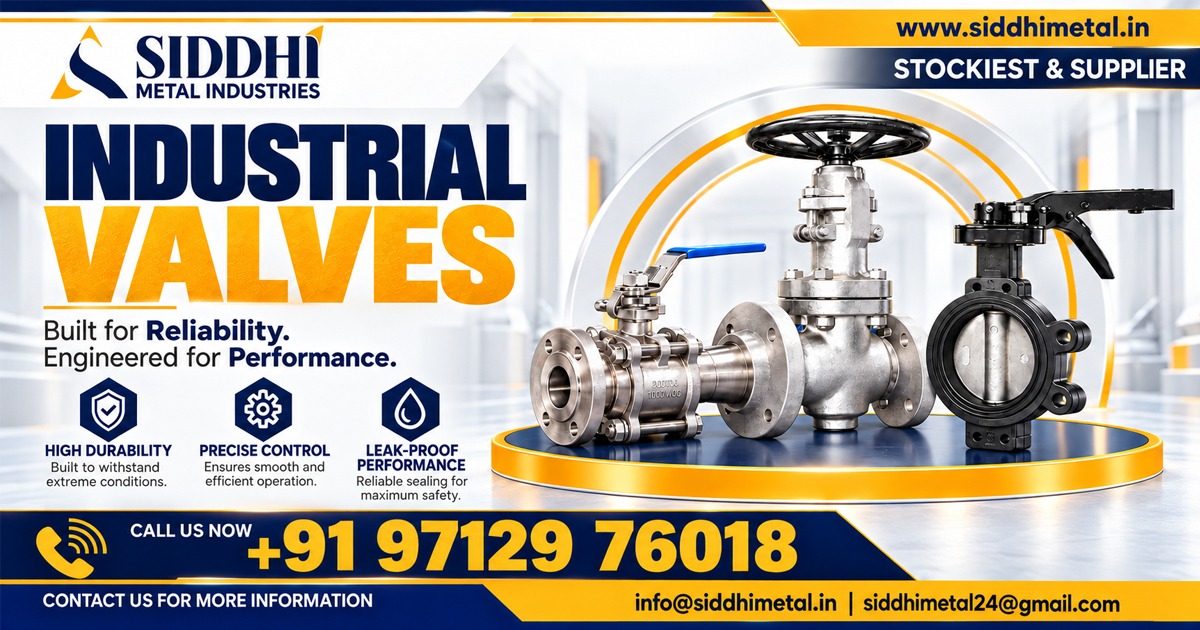
Siddhi Metal Industries is a trusted Stockiest and Supplier of Industrial Valves in Odisha, India.
Our Manufacturing unit is based in Ahmedabad, Gujarat, India.
Industrial valves play a vital role in controlling fluid movement, maintaining pressure conditions, and ensuring safe operation across industrial piping networks. From water distribution systems to high-temperature process lines, the correct valve helps industries manage liquids, gases, air, and other compatible process media efficiently.
Our industrial valve range includes Ball Valves, Gate Valves, Globe Valves, Butterfly Valves, Check Valves, Plug Valves, Diaphragm Valves, and Pressure Relief Valves. Each valve serves a specific purpose, allowing industries to select suitable equipment for isolation, flow regulation, backflow prevention, and pressure protection.
What Makes Industrial Valves Essential for Process Control?
Industrial valves regulate the movement of process media through pipelines, tanks, machinery, and equipment. Operators use them to control flow, isolate sections for maintenance, and maintain operating conditions within the required limits.
A suitable valve helps industries achieve:
• Controlled movement of liquids, gases, and steam
• Reliable isolation during maintenance
• Improved process stability
• Protection against unwanted reverse flow
• Effective management of operating pressure
• Reduced risk of leakage when correctly selected and maintained
• Better coordination between pumps, pipelines, and process equipment
Explore Eight Valve Designs for Different Operating Needs:
1. Ball Valves for Fast and Reliable Isolation
Ball valves use a rotating spherical closure element to open or close the flow passage. Their quarter-turn mechanism enables quick operation and dependable shut-off in compatible services.
Key characteristics:
• Fast opening and closing
• Compact construction
• Reliable shut-off performance
• Simple operation
• Available in varied materials and connections.
Typical uses include water supply lines, gas distribution, chemical processing, and general industrial piping.
2. Gate Valves for Pipeline Isolation
Gate valves use a gate-shaped closure element to start or stop flow. They generally perform best in fully open or fully closed positions rather than continuous throttling.
Important features:
• Suitable for pipeline isolation
• Low flow resistance when fully open
• Options for different pipeline sizes
• Robust designs for industrial service
• Construction determines pressure-temperature compatibility limits.
Industries use gate valves in water networks, power plants, utility systems, and process pipelines.
3. Globe Valves for Controlled Flow Adjustment
Globe valves regulate flow by moving a disc against a stationary seat. Their internal design makes them suitable for applications that require frequent adjustment of flow rates.
Operational advantages:
• Precise throttling capability
• Controlled flow adjustment
• Suitable for many steam and utility systems
• Available in different pressure ratings
• Effective shut-off when correctly specified
Typical applications include cooling circuits, steam lines, fuel systems, and industrial process control.
4. Butterfly Valves for Space-Efficient Installations
Butterfly valves control flow through a rotating disc positioned inside the pipeline. Their lightweight design makes them useful for many large-diameter piping systems.
Notable characteristics:
• Compact and space-saving construction
• Quick quarter-turn operation
• Lower weight than many comparable valve designs
• Convenient installation in suitable piping arrangements
• Options for water, HVAC, and compatible industrial services
Applications include water treatment, ventilation, fire protection, and industrial utility pipelines.
5. Check Valves to Prevent Reverse Flow
Check valves allow fluid to move in the intended direction and automatically restrict reverse flow when operating conditions require it.
Key functions:
• Helps prevent backflow
• Supports pump and equipment protection
• Operates without routine manual actuation
• Helps maintain the intended flow direction
• Available in different designs for specific operating conditions
Industries install check valves in pump outlets, distribution, and process pipelines.
6. Plug Valves for Straightforward Flow Control
Plug valves use a cylindrical or tapered plug with a passage through it. Turning the plug aligns or blocks the passage to control fluid movement.
Main characteristics:
• Simple operating mechanism
• Quick quarter-turn operation in suitable designs
• Effective isolation capability
• Different configurations for industrial services
• Options for selected liquid and gas applications
Plug valves serve chemical processing, petrochemical operations, and general industrial fluid-handling systems.
7. Diaphragm Valves for Demanding Fluid Services
Diaphragm valves use a flexible membrane to regulate flow and separate the process medium from certain operating components.
Practical benefits:
• Suitable for selected corrosive and aggressive media
• Minimal direct contact between the process fluid and the operating mechanism
• Effective isolation when correctly selected
• Designs that support cleaning in appropriate applications
• Options for specialised process requirements
These valves support contamination control in pharmaceutical, chemical, and water-treatment applications.
8. Pressure Relief Valves for Overpressure Protection
Pressure relief valves help protect equipment and piping systems by releasing fluid when pressure reaches a specified set point, subject to the valve design and operating conditions.
Safety-related functions:
• Helps limit excessive system pressure
• Protects suitable pressure-containing equipment
• Supports safe operation when properly sized
• Provides automatic pressure-relief action
Applications include boilers, pressure vessels, compressed-fluid systems, and industrial processing equipment.
Industries That Depend on Industrial Valve Technology:
Industrial valves support fluid management across numerous sectors:
• Oil and gas production and distribution
• Chemical and petrochemical processing
• Water supply and wastewater treatment
• Thermal and other power generation facilities
• Pharmaceutical manufacturing
• Food and beverage processing
• Industrial machinery and manufacturing plants
• Steam, compressed air, and utility systems
• HVAC and building services
• General process piping and fluid transfer
Frequently Asked Questions:
Q1. What is the main function of an industrial valve?
It controls, regulates, isolates, or redirects flow within a piping system.
Q2. Which valve is suitable for quick shut-off?
Ball valves are commonly selected for quick quarter-turn shut-off.
Q3. Which valve is best for flow regulation?
Globe valves are commonly used for throttling and controlled flow adjustment.
Q4. What information is needed to select an industrial valve?
Check the medium, pressure, temperature, valve function, material, size, and connection type.
Q5. Can industrial valves handle high temperatures?
Yes, if the valve materials, seals, pressure rating, and design are suitable for the specified temperature.
Siddhi Metal Industries is a trusted Stockiest and Supplier of Industrial Valves in Odisha, India including other locations like Angul, Boudh, Balangir, Bargarh, Balasore, Bhadrak, Cuttack, Deogarh, Dhenkanal, Ganjam, Gajapati, Jharsuguda, Jajpur, Jagatsinghapur, Khordha, Keonjhar, Kalahandi, Kandhamal, Koraput, Kendrapara, Malkangiri, Mayurbhanj, Nabarangpur, Nuapada, Nayagarh, Puri, Rayagada, Sambalpur, Subarnapur, Sundargarh, Bhubaneswar, Cuttack, Balasore, Paradeep, Balangir, Sambalpur, Berhampur, Baripada, Mayurbhanja, Keonjhar, Rourkela, Jaypore.
Email Us:
info@siddhimetal.in | siddhimetal24@gmail.com
Phone Number:
+91 97129 76018
For more information or business inquiries, we are always ready to assist you.
View Product: Click Here